
Producción de bebidas a base de plantas
No importa si se está iniciando en la producción de bebidas de origen vegetal, si desea expandir su capacidad de producción o diversificar su cartera de productos, estamos aquí para ayudarle. Con nuestros equipos, podemos ayudarle a optimizar su proceso, independientemente de sus requisitos de capacidad o materia prima. Basándonos en décadas de experiencia, le ayudamos a mejorar el sabor, la textura y la vida útil de su producto, al mismo tiempo que minimiza el CAPEX y el OPEX.
Start-ups
¿Desea crear una nueva planta de producción de bebidas de origen vegetal? Nuestros expertos en aplicaciones pueden ayudarle a seleccionar el equipo de procesamiento ideal para pasar sin problemas de las pruebas de laboratorio a la producción comercial.
Productores
Si usted es un productor de bebidas en planta que busca expandirse, factores como la limpieza, el tiempo de funcionamiento, el OPEX, el CAPEX y la gestión eficaz de los residuos tienen un impacto significativo en la rentabilidad de la planta. Con el equipo adecuado, Alfa Laval puede ayudarle a mantener la calidad del producto y garantizar un alto rendimiento de la inversión.
Lácteos
La alternancia entre leche y bebidas vegetales en su central lechera puede proporcionar nuevas fuentes de ingresos, pero también conlleva nuevos requisitos de limpieza y manipulación de residuos. Podemos ayudarle a actualizar su línea de proceso y asegurarnos de que su planta cumple todas las exigencias normativas.
Flexible processing across diverse plant raw materials
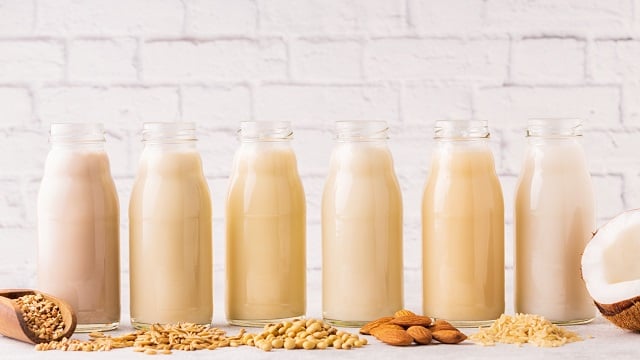
Different raw materials introduce unique processing challenges related to protein composition, starch behavior, oil content, and fiber structure. Effective plant based drinks processing adapts to these variations through tailored pretreatment, extraction, heat treatment, and separation. Equipment configurations designed for soybeans, oats, almonds, rice, coconuts, nuts, and fruit pulp enable consistent product characteristics while maximizing raw material utilization.
Process design tailored to plant-based beverage requirements
While no two production facilities are identical, plant-based drinks production generally follows a structured sequence from raw material preparation to final formulation. Process design focuses on reliability, hygienic operation, and efficient use of water and energy. Customizing each stage ensures stable performance while supporting long-term operational flexibility and consistent output quality across different plant-based beverages.

Productos



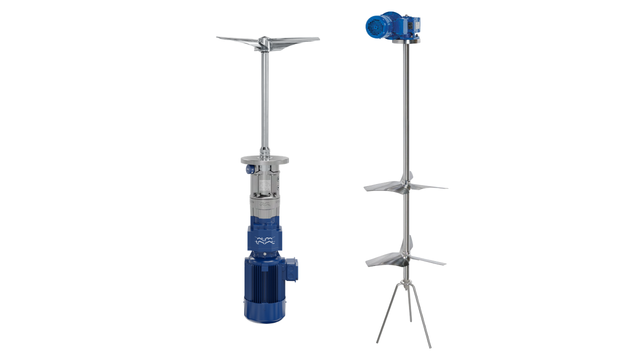


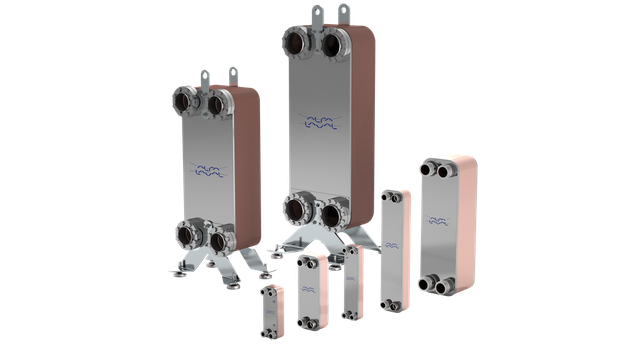
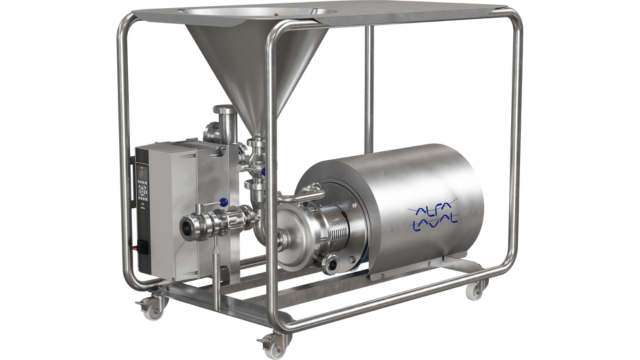
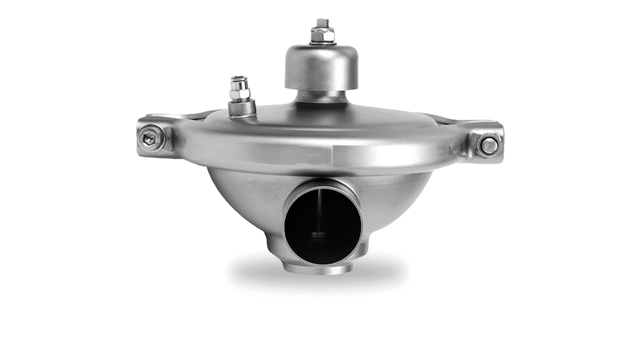
Plantastic taste. Protecting taste and texture through precise processing
The selection of equipment and process control directly influences taste, mouthfeel, and visual appearance. Accurate thermal treatment, gentle separation, and controlled mixing help preserve functional properties and prevent off-flavour or texture defects. Selecting the right heat exchangers, separation equipment, powder mixers, and flow handling equipment is critical to delivering high-quality plant protein drinks that meet market expectations.
Avoid coagulation and burnt products
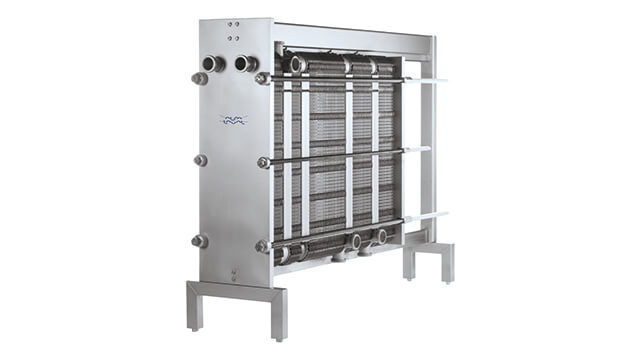
All heating and pasteurization steps risk affecting taste negatively. If the product flow is too low and the temperature too high, proteins and sugars may cause a burnt taste in your plant based drink product. We help you avoid these problems by supplying you with heat exchangers optimized for your operating conditions and raw material.
Create the perfect texture and taste of your plant-based beverages
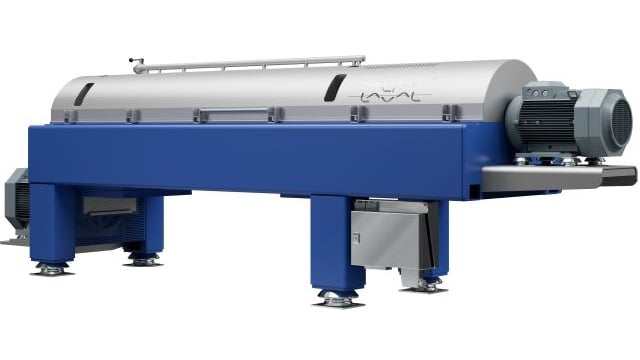
A perfect balance of solids and fats in your plant-based beverage is essential for great taste and texture, meaning separation stages are critical for product quality. We help you select the right separation equipment for your process, ensuring both high performance and sustainability.
Ensure hygiene and product safety
Spotless processing equipment is essential for both food safety and taste. Choosing inadequate equipment puts you at risk for cross-contamination between batches and residues of cleaning chemicals. The smooth surfaces and hygienic design of all Alfa Laval food processing equipment ensure it is easy to clean and that no residues remain after CIP.
Sustainable plant-based solutions for long-term competitiveness
Sustainability has become a defining factor in plant-based drinks production as customers increasingly evaluate environmental performance. Efficient plant-based solutions help reduce energy consumption, water usage, emissions, and waste without compromising product quality. Process optimization supports compliance with regulatory requirements while strengthening sustainability credentials across global supply chains.
Energy savings
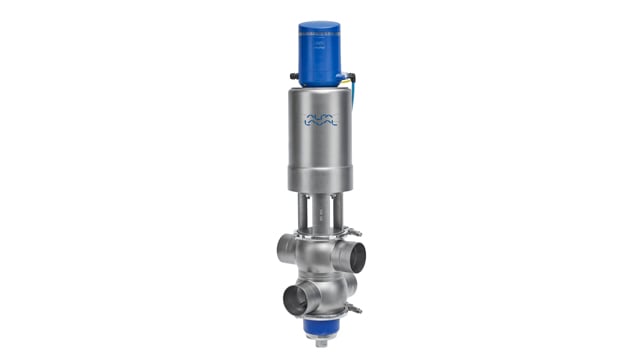
Our unique pump and valve solutions not only use minimal electrical power during operation, but also enable substantial reductions in hot-water consumption thanks to Alfa Laval's unique burst seat cleaning technology. Alfa Laval heat exchangers also offer up to 94% heat recovery when you recover and reuse energy from hot process streams to save steam.
Water savings
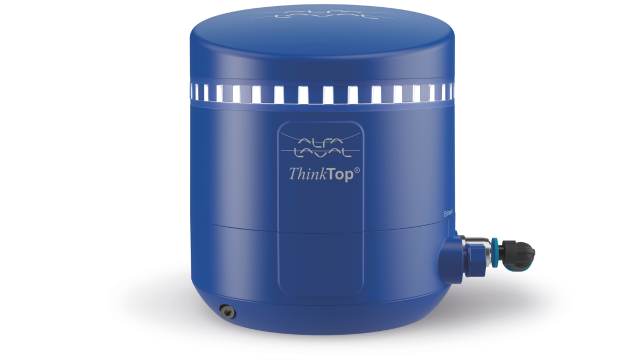
Environmental impact and water conservation has become integral in sustainable business strategies for companies, large and small. Using Alfa Laval Unique Mixproof valves and ThinkTop control units, you can save up to 90% of the water and chemicals used during cleaning.
Waste reduction
Together with your preferred integrator, we can supply complete, customized treatment plants for industrial wastewater, and help you reduce your waste to a minimum, recover valuable by-products, and even implement zero-liquid-discharge (ZLD) solutions.
Transportation savings
If you are an ingredients manufacturer producing base liquids, there are great savings to be made in transport-related emissions and costs if you concentrate your product before shipping. At Alfa Laval, we have extensive experience supplying systems based on evaporation or membrane technology. We can help you find the optimum solution based on your requirements and operating conditions.
Professional support right from the start
Backed by experience in servicing equipment for food, dairy & beverage applications, we are ready to support you whenever you encounter problems or wish to discuss upgrade opportunities in your dairy beverage production. We specialize in optimizing CIP programs to reduce water consumption and use of cleaning agents. Thanks to our global network of partners, field service engineers, service centers and spare parts distribution hubs, qualified help and genuine spare parts are always available.
We can support you from the initial installation and commissioning stage, and throughout the entire lifetime of your equipment with preventive maintenance, upgrades, remote monitoring, predictive maintenance, troubleshooting, and more.
Ensure maximal uptime, performance and return on investment. Learn more about the services we offer:
Decanter centrifuge services Hygienic pump services Heat exchanger services
Hygienic tank equipment services Hygienic valve services
Customer stories
Introducing a new heat treatment technology for oat beverage
When a liquid food producer in northern Europe was looking to replace an existing heat exchanger, which they used for heating up oat-based, they deviated from the conventional path by not choosing a shell & tube solution. Instead, they chose an HL8-WG from Alfa Laval’s Hygienic line.
Photo courtesy of Meadow Foods